If your orders are growing, you likely ask: should we buy a paper cup machine and die cutting machine at once, or first expand the forming line and defer die cutting? This is the most common decision point when moving from one machine to a fuller workflow.
This guide is for buyers evaluating whether adding paper cup machine and die cutting machine integration improves profit and delivery consistency, or only increases workload and maintenance risk. The answer is almost always “it depends”, but not in a random way. It depends on your order mix, rejection profile, print complexity, and whether your bottleneck is currently upstream or downstream.
We will evaluate practical buyer scenarios, not brochure comparisons. The goal is to avoid over-investment while locking in order reliability, profit, and upgrade pace.
Why buyers face the same upgrade question
A forming line can start generating sales quickly. Then many buyers feel confident and add die cutting, printing, and packing in a short sequence. A few months later, they discover that order acceptance is still blocked by another stage. The same issue repeats because the upgrade was not linked to a measured bottleneck.
As a practical rule, upgrade decisions should follow measurable blockers, not competitor claims or model specs alone. If the blocker is unstable fan supply and high rework at die edges, die cutting is likely useful. If the blocker is packing and counting delay, the first upgrade should be downstream even if die cutting seems attractive.
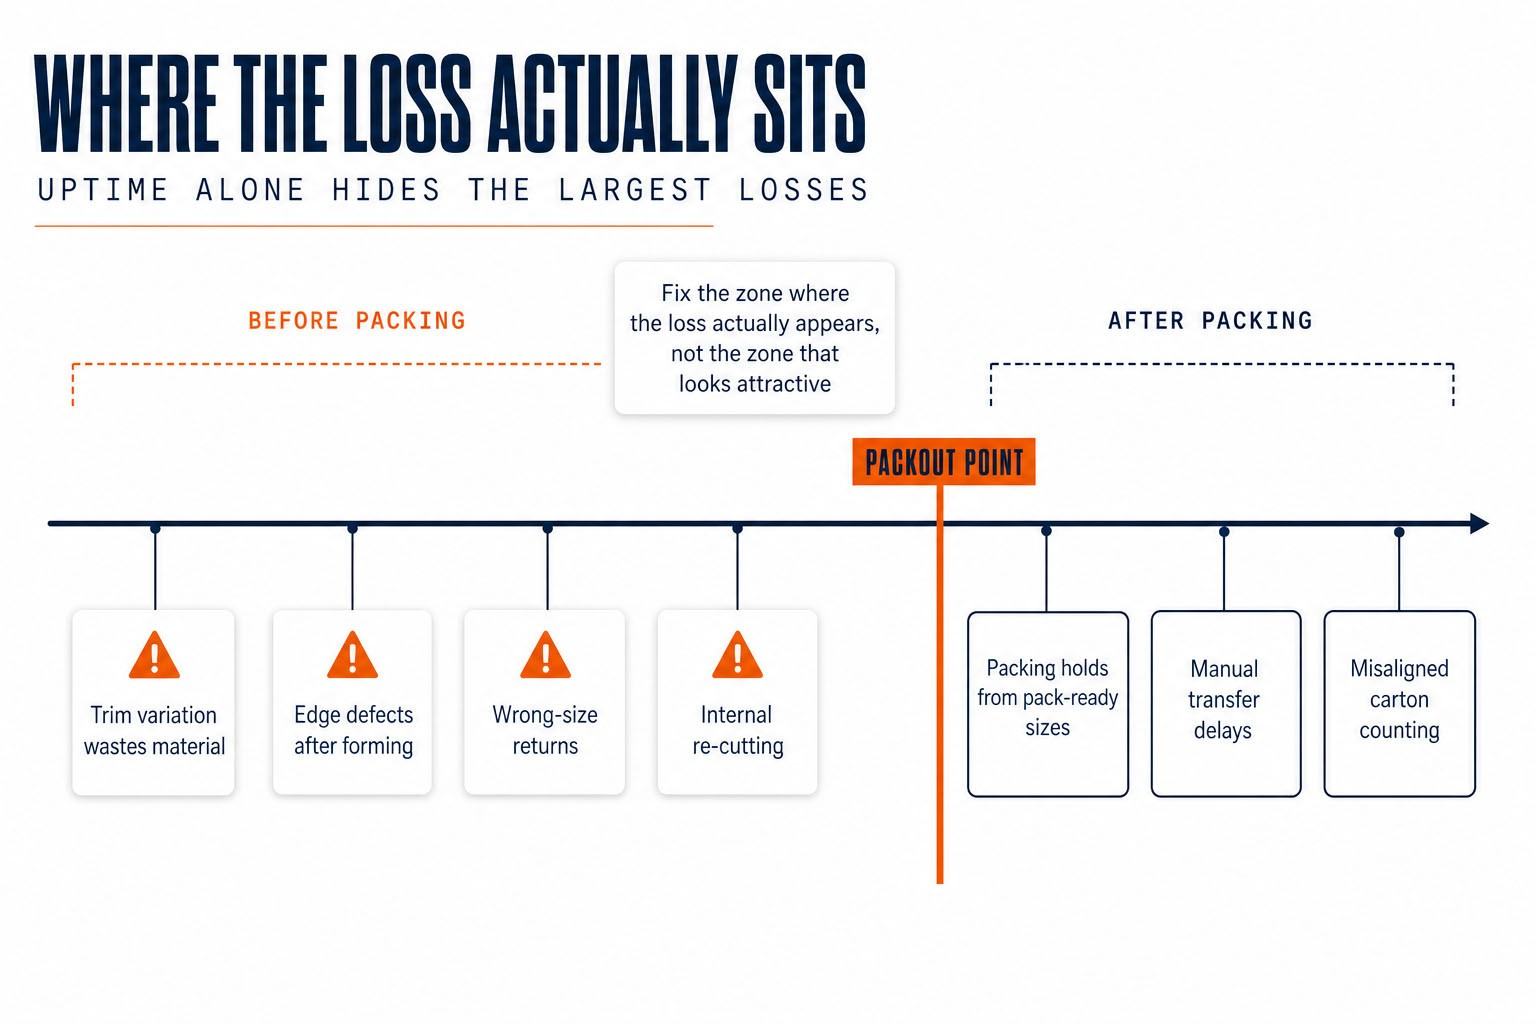
This is why this article separates three questions:
- Does current output quality justify in-house die cutting control?
- Will the upgrade reduce the highest delay cost line in your workflow?
- Can your team absorb technical complexity without hurting delivery confidence?
Only when all three are answered positively does the upgrade usually pay off in the first 6-12 months.
What a paper cup machine and die cutting machine setup means
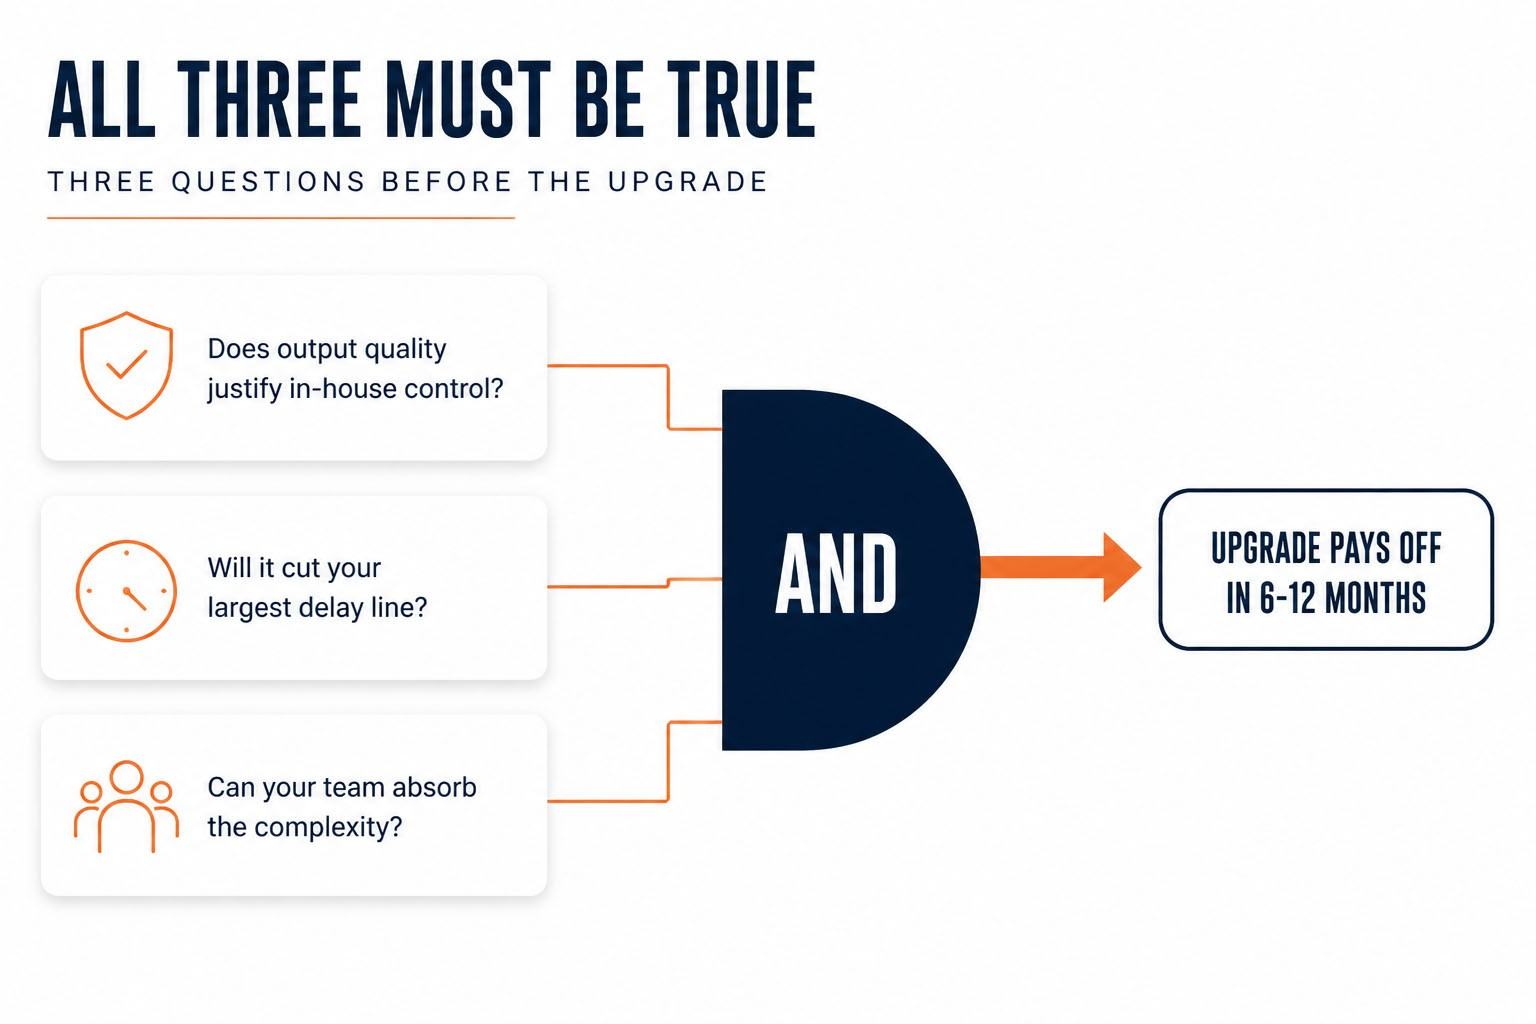
Many buyers think a paper cup machine and die cutting machine is only for print-heavy brands. In reality, it is a control layer in your chain. It helps you own shape consistency and timing at source, but it also adds responsibility for raw material prep and quality gates.
A practical production chain to keep in mind:
material intake -> printing -> die cutting -> forming -> inspection -> paper cup packing machine -> shipping. If upstream variation is high, die cutting controls variation for you. If upstream is stable, it may become optional in early stage.
For buyers using paper cup fan from external suppliers and low design complexity, forming plus disciplined fan QC often performs better than a full in-house setup at first.
For buyers with frequent brand variants, variable cup sizes, and strict delivery windows, the logic can flip: die cutting reduces rework and schedule drift. That is usually the point where integration begins to create real margin.
Where cost and delay losses really happen
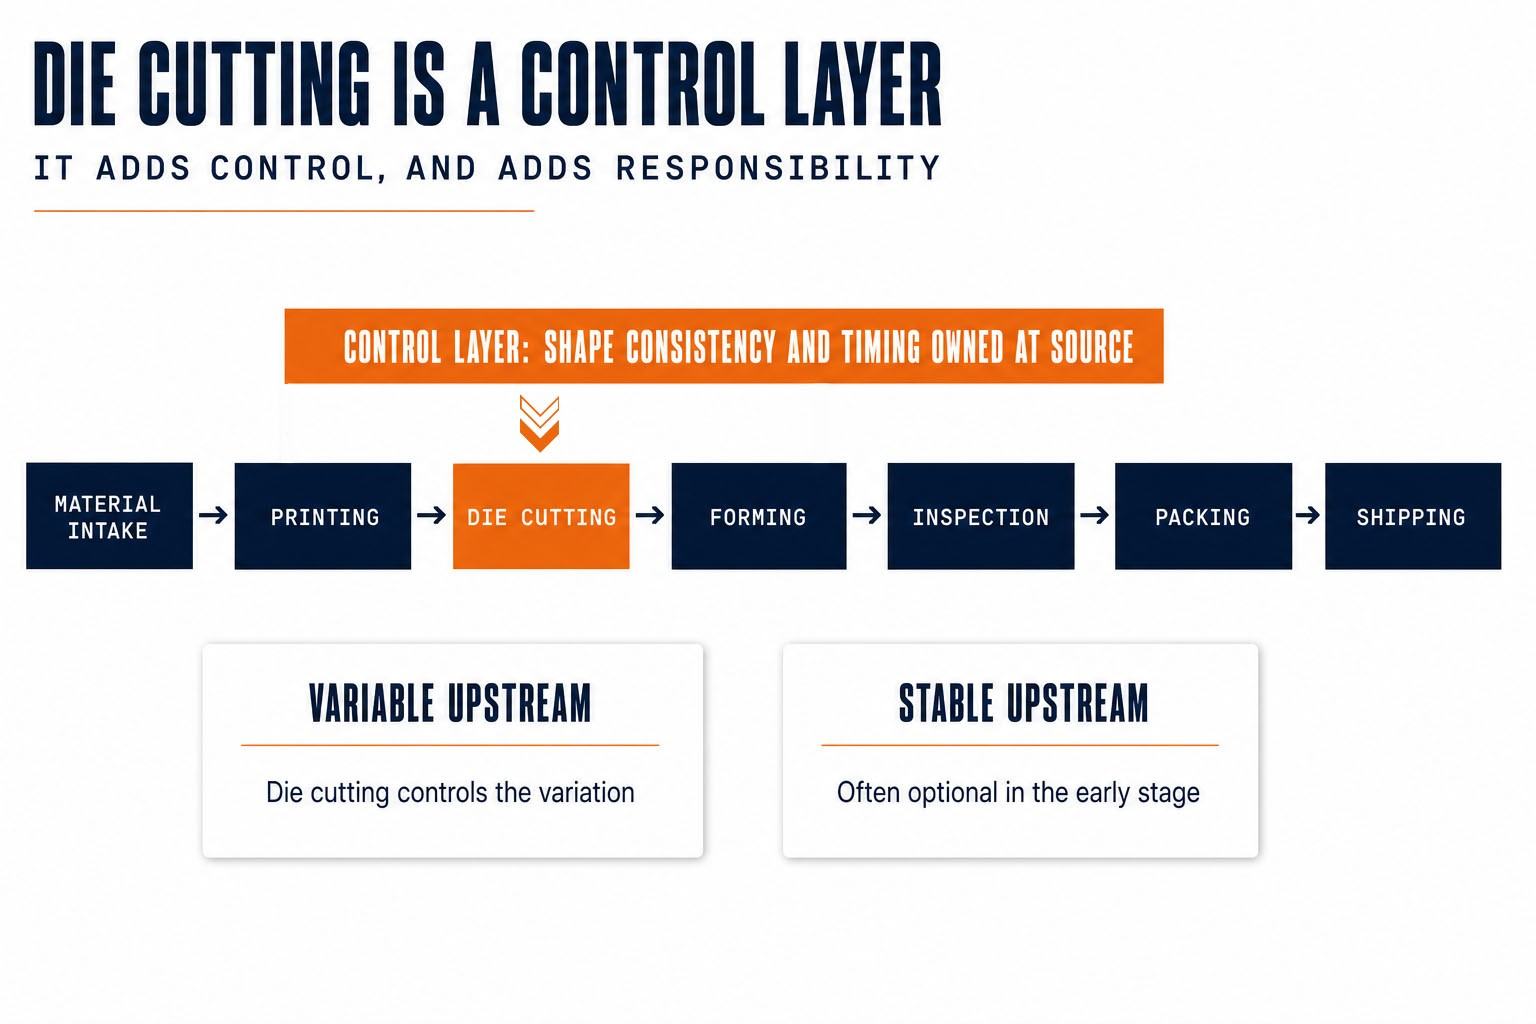
Before investing, map where losses occur. Many buyers track machine uptime only. That misses the largest losses:
- Lost materials from trim variation.
- Rework from edge defects after forming.
- Packing holds caused by inconsistent pack-ready dimensions.
- Dispatch delay caused by manual transfer or misaligned carton counting.
Rule of thumb: if your rejection or rework happens before packing, die cutting control is directly relevant; if it happens after packout, your bottleneck is not yet solved.
| Loss source | Typical symptom | Most relevant upgrade |
|---|
| Material inconsistency | Different edge cut quality across lots | Paper cup machine and die cutting machine integration |
| Frequent reprints | Short lead time misses, repeated mockups | Printing and die-cutting process standardization |
| Packing congestion | Finished cups waiting for count/pack | Downstream automation before upstream expansion |
This table is useful because it prevents “first machine” decisions from ignoring chain-level pressure. You upgrade the stage that is blocking cash flow and customer service first.
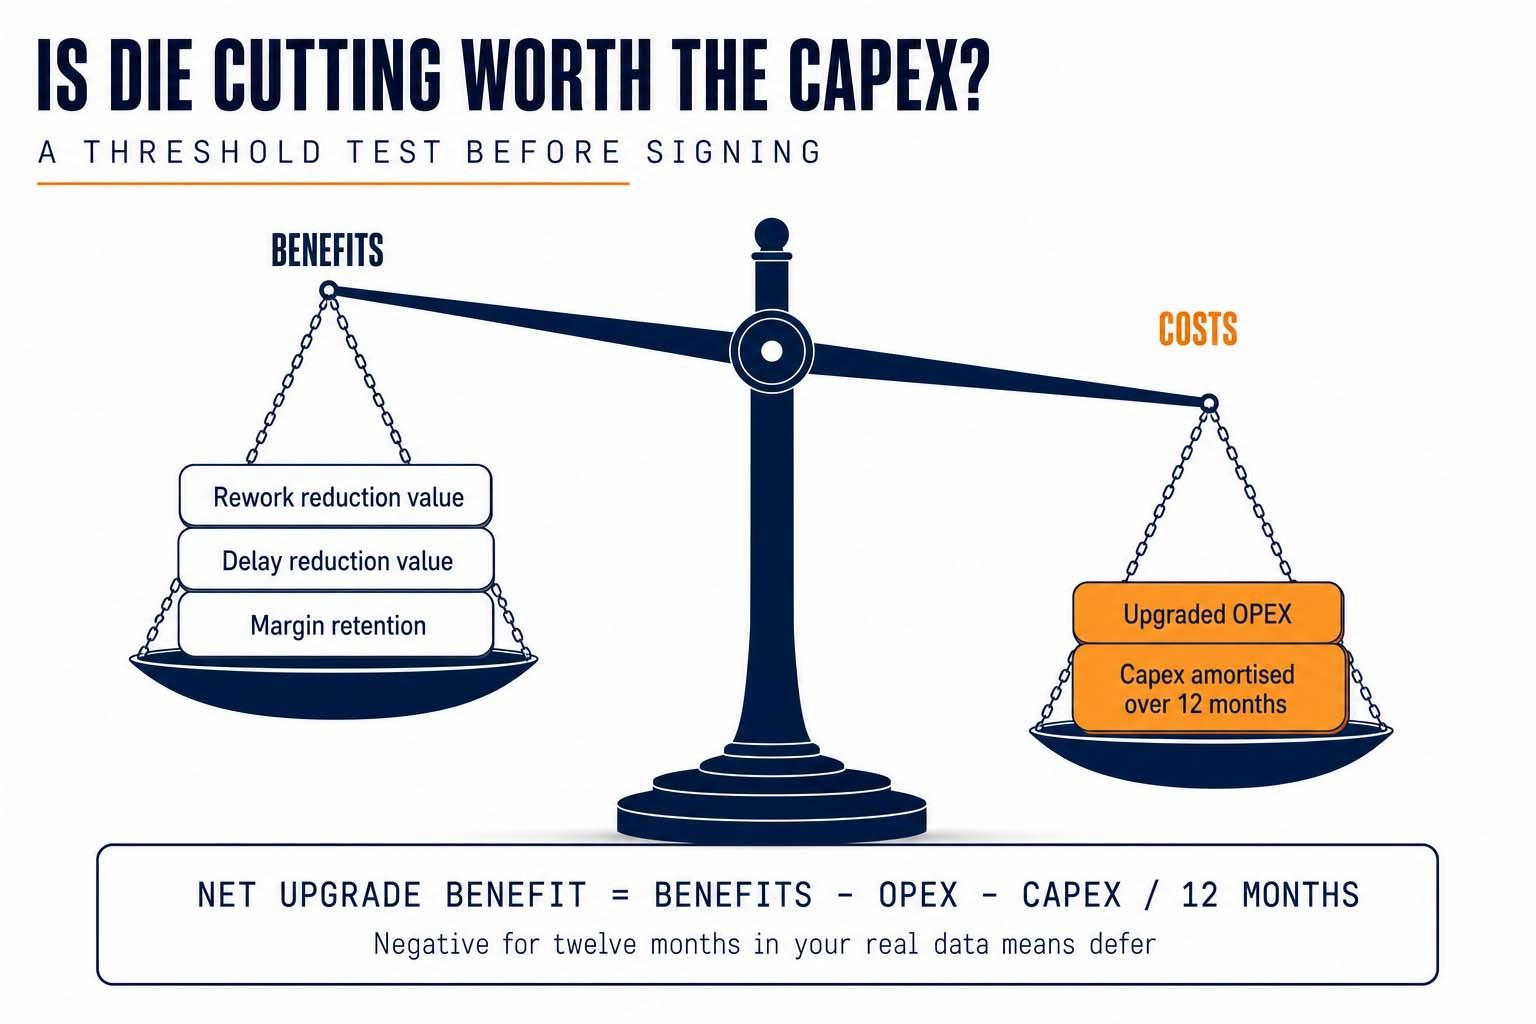
Use a simple threshold model before signing. If this model is not met, keep your upgrade staged.
Decision formula:
Net Upgrade Benefit = (Rework Reduction Value + Delay Reduction Value + Margin Retention) - Upgraded OPEX - Capex amortized in 12 months
Rework Reduction Value is usually from lower defect scrap, fewer wrong-size returns, and reduced internal re-cutting. Delay Reduction Value comes from shorter order lock-to-ship time and fewer emergency rescheduling costs.
A practical trigger is simple: if the model is negative for 12 months in your real data, defer in-house die cutting and continue with controlled external sourcing.
A related operational formula is useful for daily control:
Net Available Capacity = Forming Throughput - Upstream Rework Loss - Packing Delay Loss
If rework and packing delay are both high, capacity gains from adding machine count are diluted. In many cases, die cutting investment should be delayed until one of these two losses is proven and reduced.
Buy-ready fan vs in-house die cutting: comparison
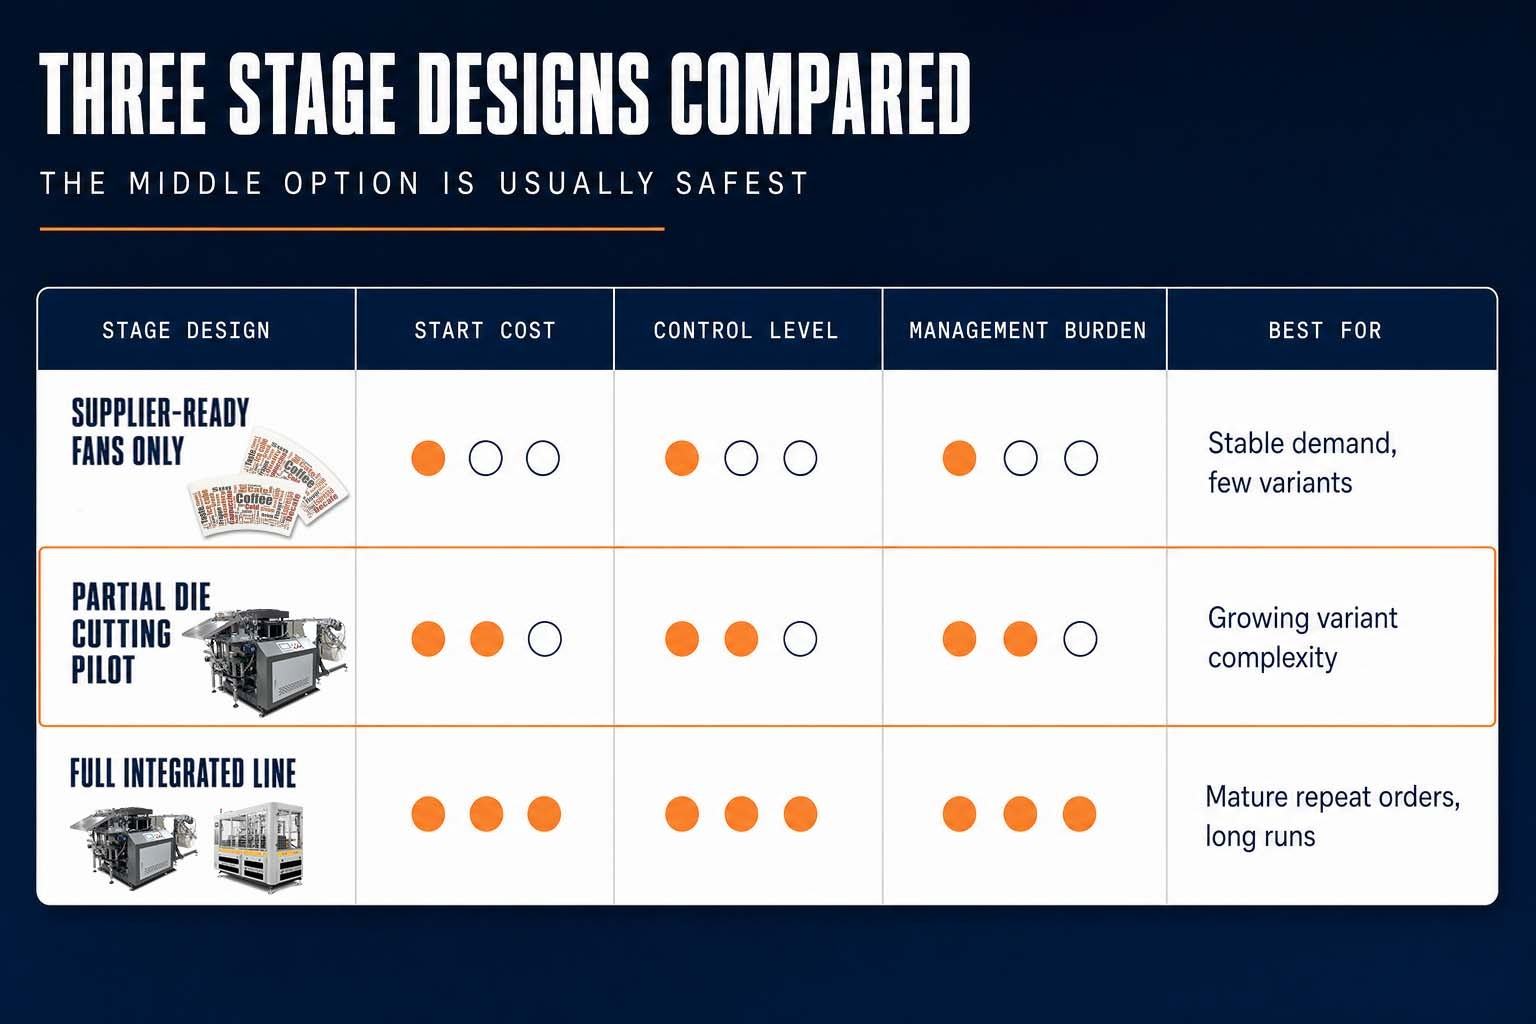
For many small-to-mid factories, the first choice is between stable supplier support or vertical control. The right answer is rarely all in.
| Stage design | Start cost | Control level | Management burden | Best for |
|---|
| Supplier-ready fans only | Low to medium | Lower | Lower | Stable demand, few variants |
| Partial die cutting (pilot) | Medium | Medium | Medium | Growing variant complexity |
| Full integrated paper cup printing die cutting forming line | High | High | Higher | Mature repeat orders and long run stability |
The middle option is often safest: pilot one die cutting station after three quality checkpoints are already in place at forming and inspection.
A practical note from the market: buying only for capability without process discipline will not increase throughput. Capability is valuable only if your team can hold repeat tolerances.
Upgrade path by buyer type
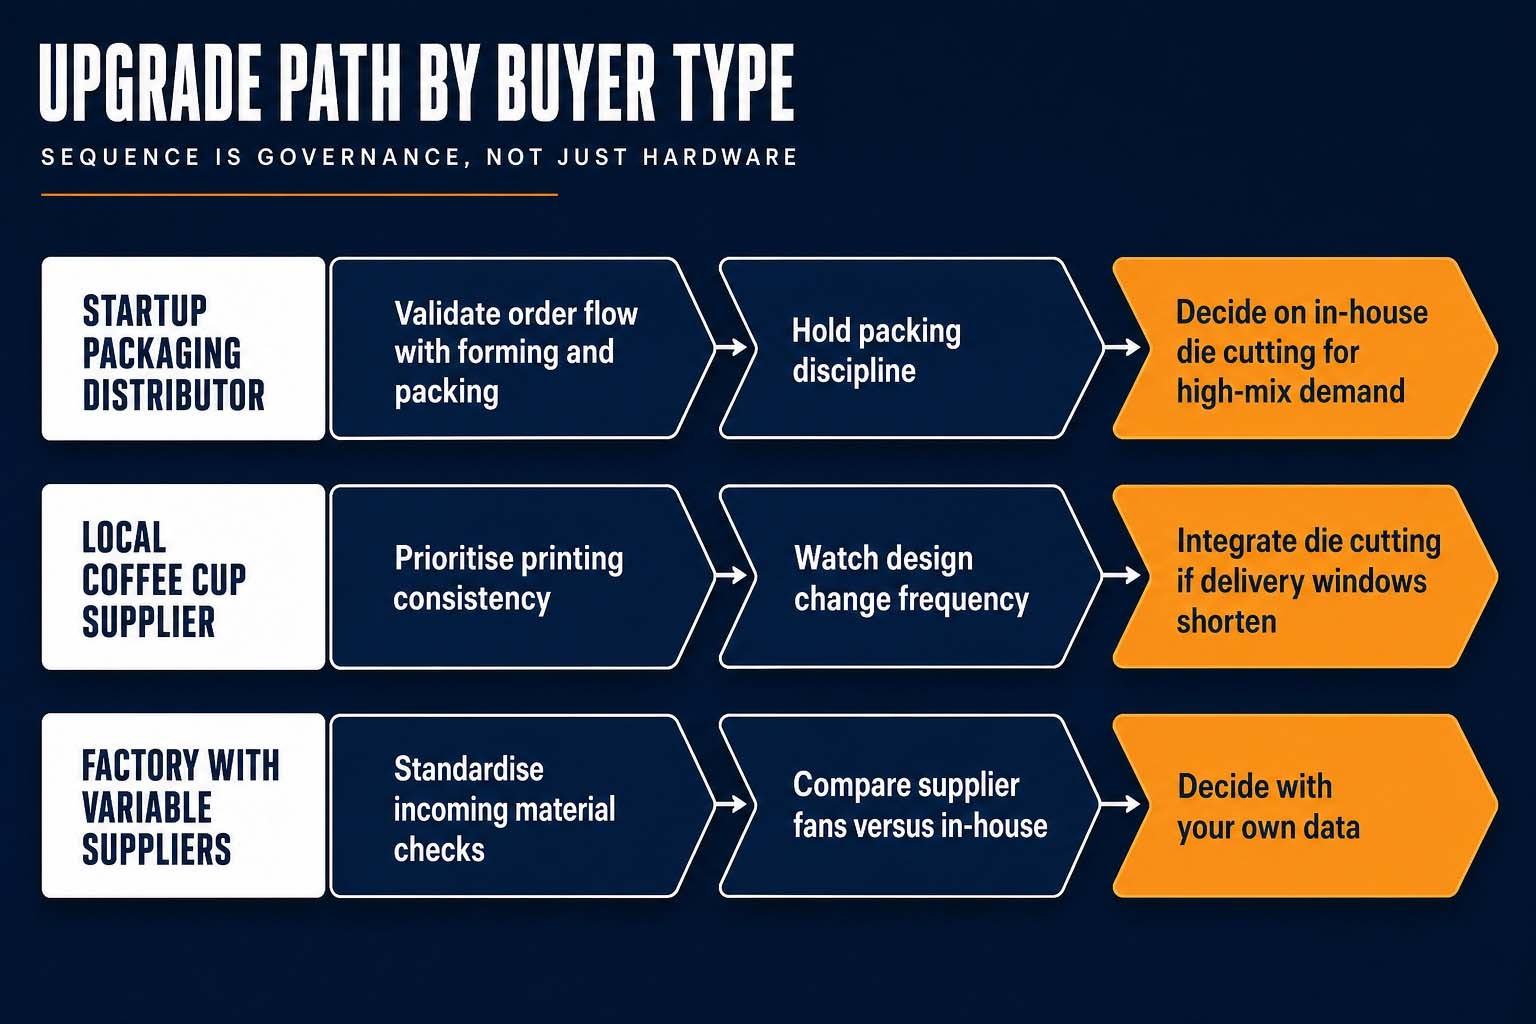
Use the following path by buyer intent:
- Startup packaging distributor: validate order flow with forming + packing discipline first, then decide on in-house die cutting for high-mix demand.
- Local coffee cup supplier: prioritize printing consistency, then integrate die cutting if design changes reduce delivery windows.
- Existing factory with variable suppliers: standardize incoming material checks first, then compare supplier-led fans versus in-house die cutting using your own data.
If your long-term plan includes premium segments, include paper cup die cutting machine capability in your roadmap, but only after baseline controls are stable.
This is the part many buyers miss: upgrade sequence is a governance decision, not just hardware acquisition.
90-day to 12-month investment timeline
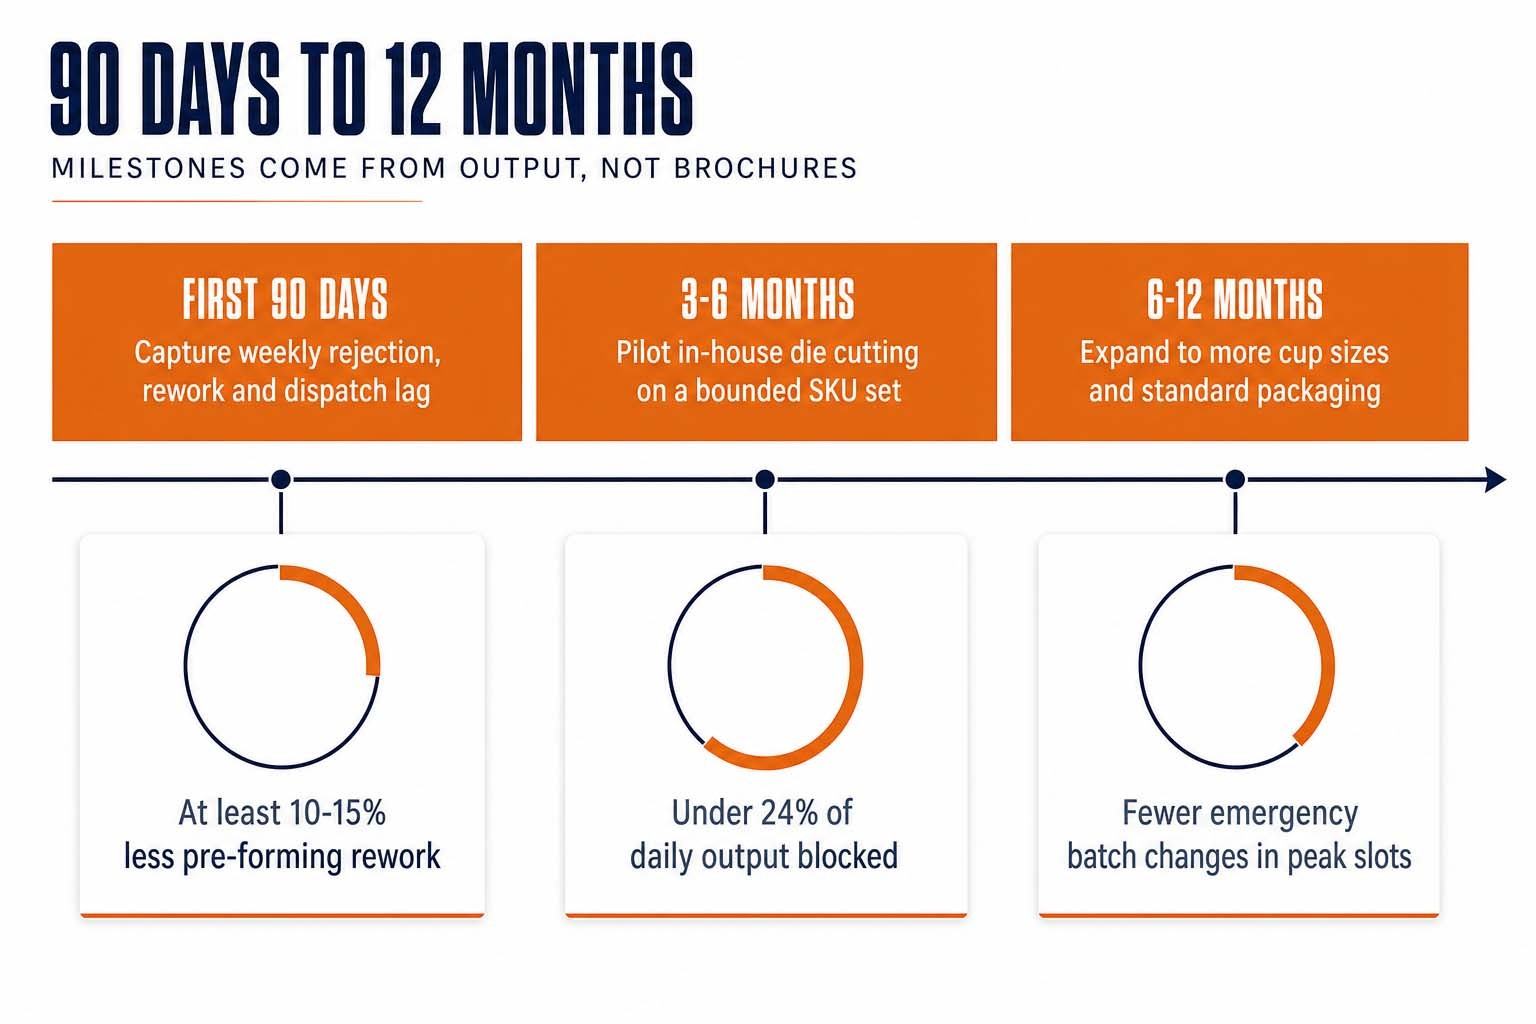
First 90 days: build baseline using current line, capture weekly rejection, rework, and dispatch lag. If these are stable, proceed to controlled pilot.
3-6 months: pilot in-house die cutting for a bounded SKU set. Compare defect trend and lead-time variance against the control lot.
6-12 months: if pilot shows measurable improvement, expand to additional cup sizes and integrate standard packaging flow for those SKUs.
This timeline avoids early overrun. Upgrade milestones are not based on model brochure specs. They are based on measurable outputs:
- At least 10-15% reduction in pre-forming rework ratio.
- Less than 24% of daily output blocked by non-upstream bottlenecks.
- Reduced emergency batch changes during peak slots.
For high-mix customers, this staged path also supports workforce readiness. You avoid a capability gap where people are responsible for more stages than their training allows.
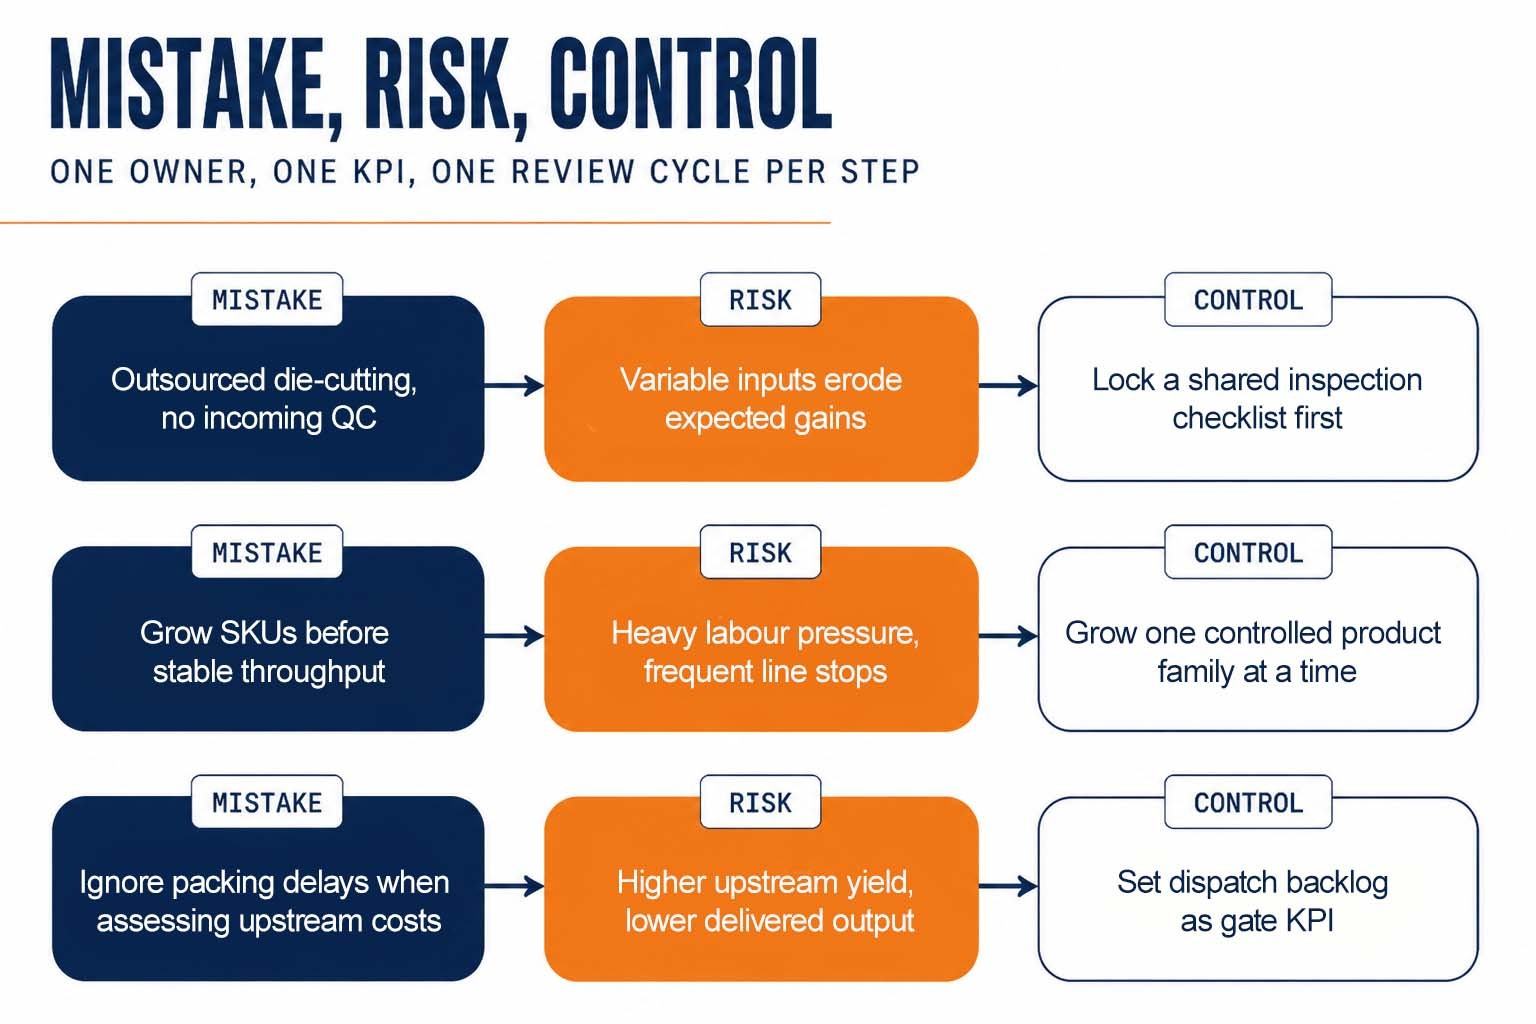
Common upgrade mistakes and control points
- Mistake: Buying die cutting and printing without standardized incoming quality gates.
- Risk: Inconsistent input quality erodes any expected gain.
- Control: lock a shared inspection checklist before upgrade.
- Mistake: Expanding SKU count before throughput data is stable.
- Risk: high labor pressure and frequent line stops.
- Control: limit expansion to one controlled family at a time.
- Mistake: Ignoring packaging delay when evaluating upstream investment.
- Risk: higher upstream output but lower delivered output.
- Control: use dispatch backlog as one of your gating KPIs.
Decision warning: if you see higher output on the machine but lower on-the-road dispatch, you have solved the wrong problem.
Most upgrade failures come from adding technical steps without adding responsibility and tracking points. That is why each new equipment step should have one owner, one KPI, and one review cycle.
Pre-upgrade decision checklist
Before investing in paper cup machine and die cutting machine integration, confirm all items:
- Average monthly order quantity by SKU and repeat order ratio.
- Current rework percentage and top three defect causes.
- Mean order lead-time target and current deviation.
- Material acceptance pass rate for incoming paper cup fan.
- Manual packaging backlog by day.
- Cash reserve for a 3-6 month stabilization period.
- Availability of process operator and maintenance coverage.
If more than two points are weak, delay the upgrade until the chain is operationally ready. This protects margin and avoids urgent troubleshooting from dominating your launch period.
FAQ for this upgrade decision
1. Can a startup skip die cutting and still stay competitive?
Yes, if demand is predictable and design changes are limited. A strong forming process plus controlled fan procurement can handle early-stage operations.
2. When is die cutting most valuable?
When repeat redesigns and size changes create frequent delays, and rework starts to eat your margin. In that case, control at cut stage gives stronger order reliability.
3. Should we buy only one die cutting machine?
Start with one controlled station and a bounded SKU list. Expand only when utilization and quality KPIs stay stable for several cycles.
4. Is in-house die cutting always better than supplier-ready fan?
No. It is better only when the hidden cost of delays, reworks, and coordination outweighs the added complexity.
5. What about premium premiumized products?
For premium products with strict graphics and frequent SKUs, this upgrade may shorten cycle time and reduce returns, but only if your process team can hold tighter tolerances.
The Bottom Line
Decision rule: a paper cup machine and die cutting machine upgrade is strategic only when upstream quality loss and lead-time volatility are the real bottlenecks.
For many buyers, the right sequence is: stabilize daily operating discipline, verify paper cup fan consistency and packing readiness, then scale with pilot-controlled die cutting. This sequencing protects working capital and supports repeatable margin.
Next step: if you want, we can help you map your real production data into the upgrade formulas above and identify the first KPI-based milestone for your next machine decision.

 Tel: +86-13362708280
 Email: george@paper-cupmakingmachine.com
 MP/WhatsApp: +86-13362708280
 Manufacturer Address:No.1588, Huaming Road, Feiyun Street,Ruian City Zhejiang Province -325200 China